
Description
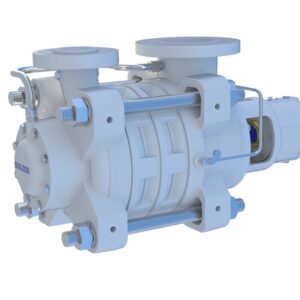
Kelair MBN high pressure stage casing pump isa horizontal, radially split, multistage ring-section pump designed for high-pressure applications. It is widely utilized across various industries for pumping clean or slightly polluted hot or cold liquids.
Key Applications
-
- Power Generation: Boiler feed duties and condensate service.
- Water & Desalination: High-pressure reverse osmosis (RO) membrane feed, and municipal water supply.
- General Industry: High-pressure water, paper mill shower water, and mine dewatering.
Design & Engineering Features
- Modular Construction: Features axially integrated diffusers and a segmental ring-section casing.
- Keyless Polygon Shaft: Ensures equal torque transmission to impellers, reduces stress points, and maintains shaft straightness.
- Axial Thrust Balancing: Employs a balance drum or balance disc to manage axial thrust loads under extreme operating conditions, extending the pump’s lifespan.
- Materials: Casing and impellers are available in a wide range of materials, including chromium steel, duplex, and super-duplex stainless steel for abrasive or corrosive environments.
- Easy Maintenance: The bearing units and mechanical seals are easily accessible and serviceable without disassembling the entire pump.